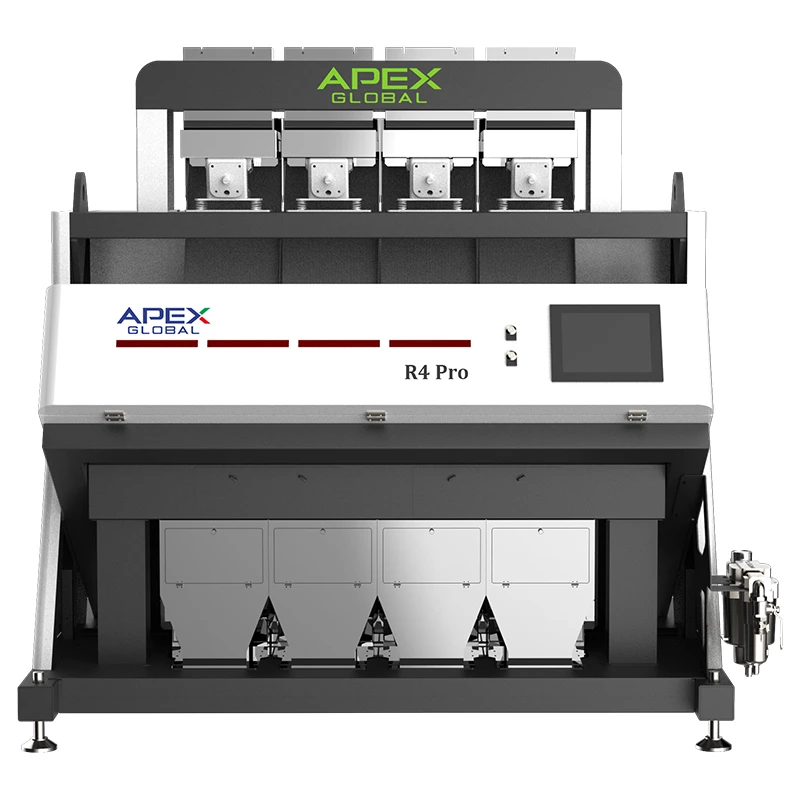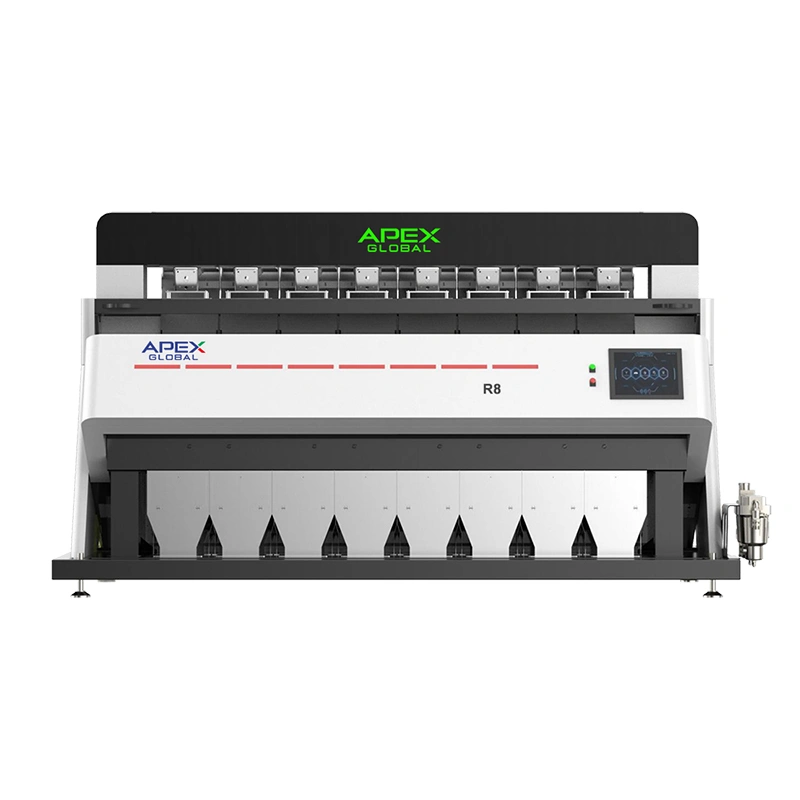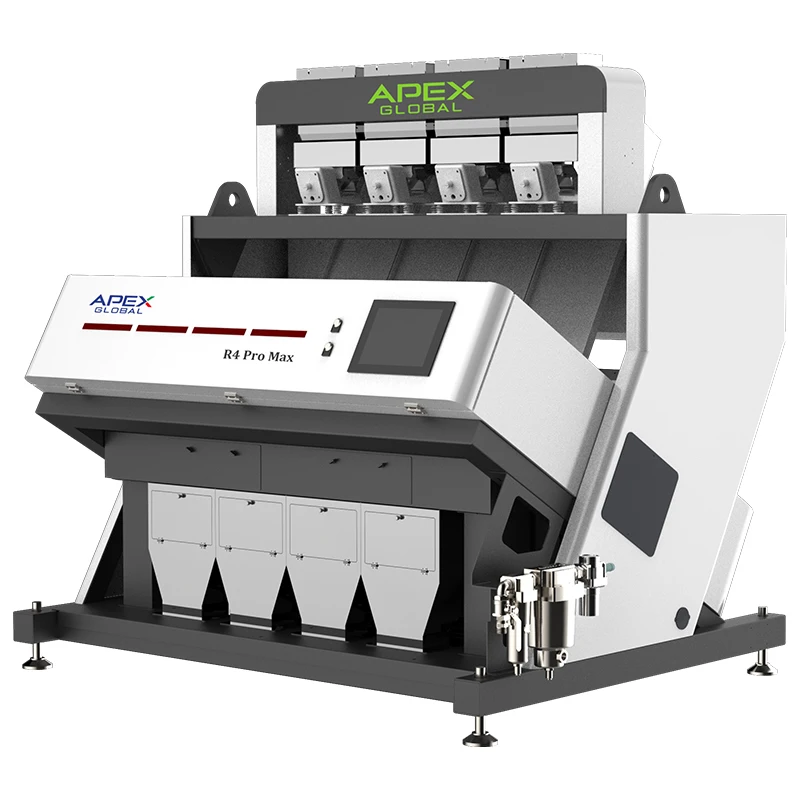



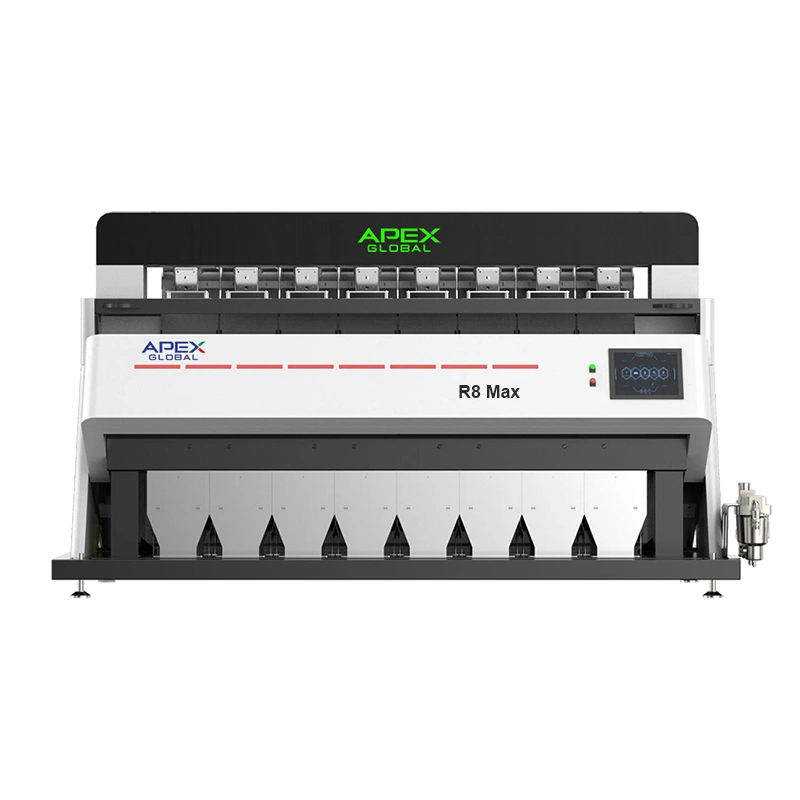
R MAX Series Industrial High-Throughput Vertical Rice Color Sorter Machine
Specs & Features: Industrial multi-channel high-flow CCD sorting system, matchable industrial-grade AI deep learning module
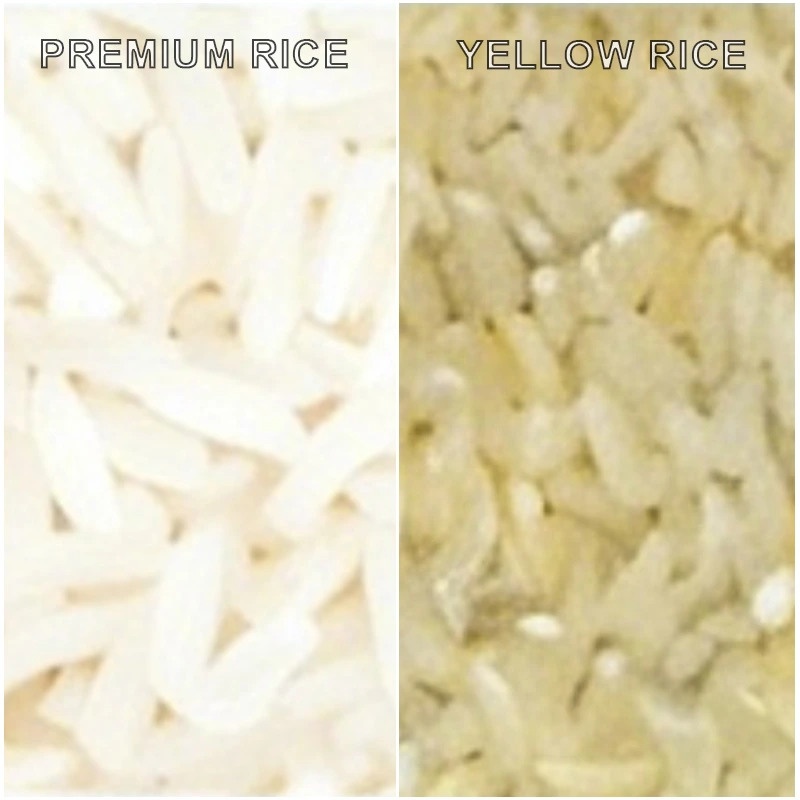
APEX Paddy Rice Color Sorter Machine of Yellow/Chalky Rice Removal
Key Advantages
- Ultra-high Throughput for Industrial Mass Manufacturing
- Heavy-duty Reinforced Structure with Excellent Anti-blocking Performance
- Optional Industrial AI Algorithm for High-fidelity Precision Sorting
- On-board Intelligent Early Warning System for Stable Continuous Operation
Products Center
Contact Us
- Phone: +86 18815515040
- Email: info@apexitec.com
- WhatsApp: +86 18815515040
- Address: No. 789 Mingchuan Road, Boyan Tech Park, Hefei, Anhui, China
Product Introduction
APEX Rice Color Sorter Machine Features
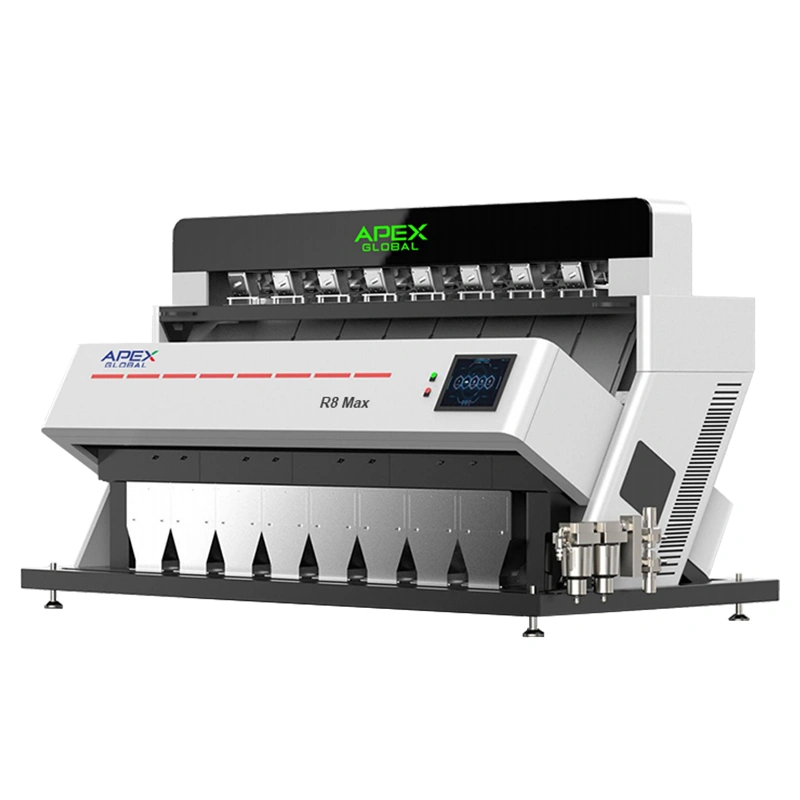
The R MAX rice color sorter is industrial-grade high-throughput optical sorting equipment custom-built for large rice milling conglomerates and fully automated high-capacity rice processing production lines. It effectively eliminates the output limitation of conventional medium and small-scale color sorting devices. While inheriting professional grain recognition precision tailored for rice characteristics, the unit realizes mass-volume, high-efficiency rice purification with minimized unplanned downtime for industrial continuous production scenarios.
1. Ultra-high Throughput for Industrial Mass Manufacturing
Fitted with an enlarged heavy-duty feeding assembly and multi-channel parallel CCD detection arrays, the equipment achieves remarkable hourly processing capacity. It supports round-the-clock non-stop bulk processing for multiple rice categories covering premium long-grain white rice, brown rice, parboiled rice and glutinous rice, perfectly matching the continuous operating rhythm of large centralized rice processing bases.
2. Heavy-duty Reinforced Structure with Excellent Anti-blocking Performance
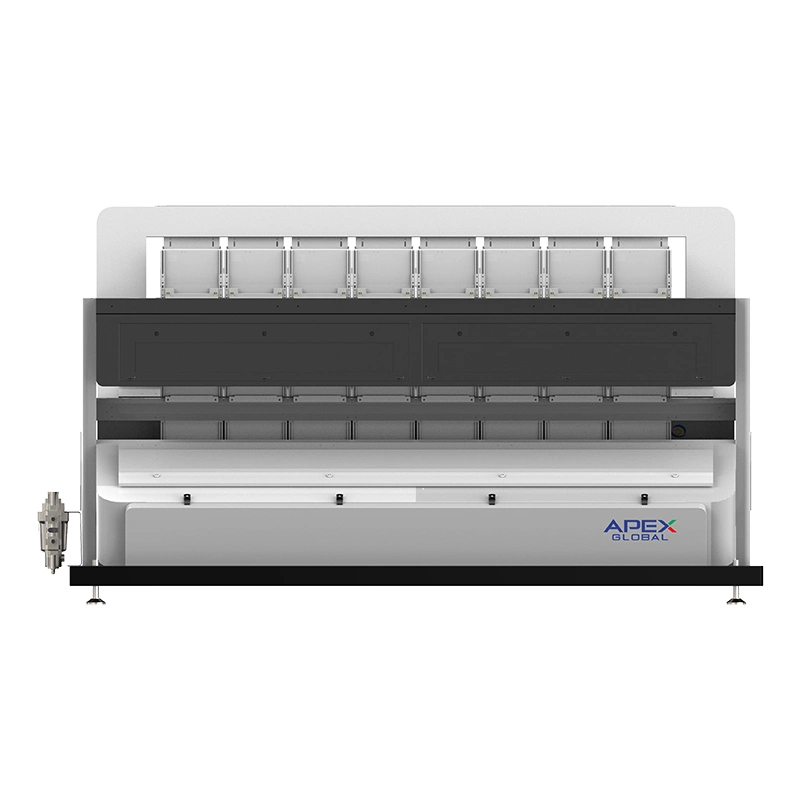
The industrially strengthened chute framework paired with a calibrated stable vibration feeding mechanism thoroughly avoids material buildup, grain bridging and feed jamming under maximum material throughput. It sustains consistent sorting precision and stable detection performance throughout prolonged high-load industrial operation, eliminating accuracy drift caused by long-hour overload work.
3. Optional Industrial AI Algorithm for High-fidelity Precision Sorting
Clients are allowed to deploy industrial-level rice-oriented deep learning AI modules based on actual raw material complexity and finished rice quality requirements. The intelligent algorithm makes up for the inherent fine-defect identification defects of traditional high-output sorters, removing micro impurities and subtle flawed grains thoroughly without compromising overall production throughput.
4. On-board Intelligent Early Warning System for Stable Continuous Operation
Embedded real-time equipment status monitoring plus intelligent early warning & fault prompt systems drastically reduce manual on-site supervision and unexpected line shutdown failures. It supports standardized, low-operation-cost and high-efficiency quality improvement for large-volume rice finished products.
Purpose-engineered for large rice milling plants and fully automatic industrial production pipelines, the R MAX high-capacity rice color sorter delivers dependable high-yield sorting solutions for bulk rice purification and large-scale industrial rice quality upgrading projects.
Parameters of Rice Color Sorter Machine
| Model | Ejector No. | Power(kW) | Air Pressure(MPa) | Air Consumption(m³/min) | Weight(kg) | Dimension(mm) |
| R MAX Series | 320~1024 | 2.2~6.5 | 0.6-0.8 | ≤3.5~10.0 | 1350~3200 | Customizable |
Mass Sorting Effect & Multi-Material Adaptation Verification
Actual Separation Performance for Bulk Rice & Grain Industrial Processing
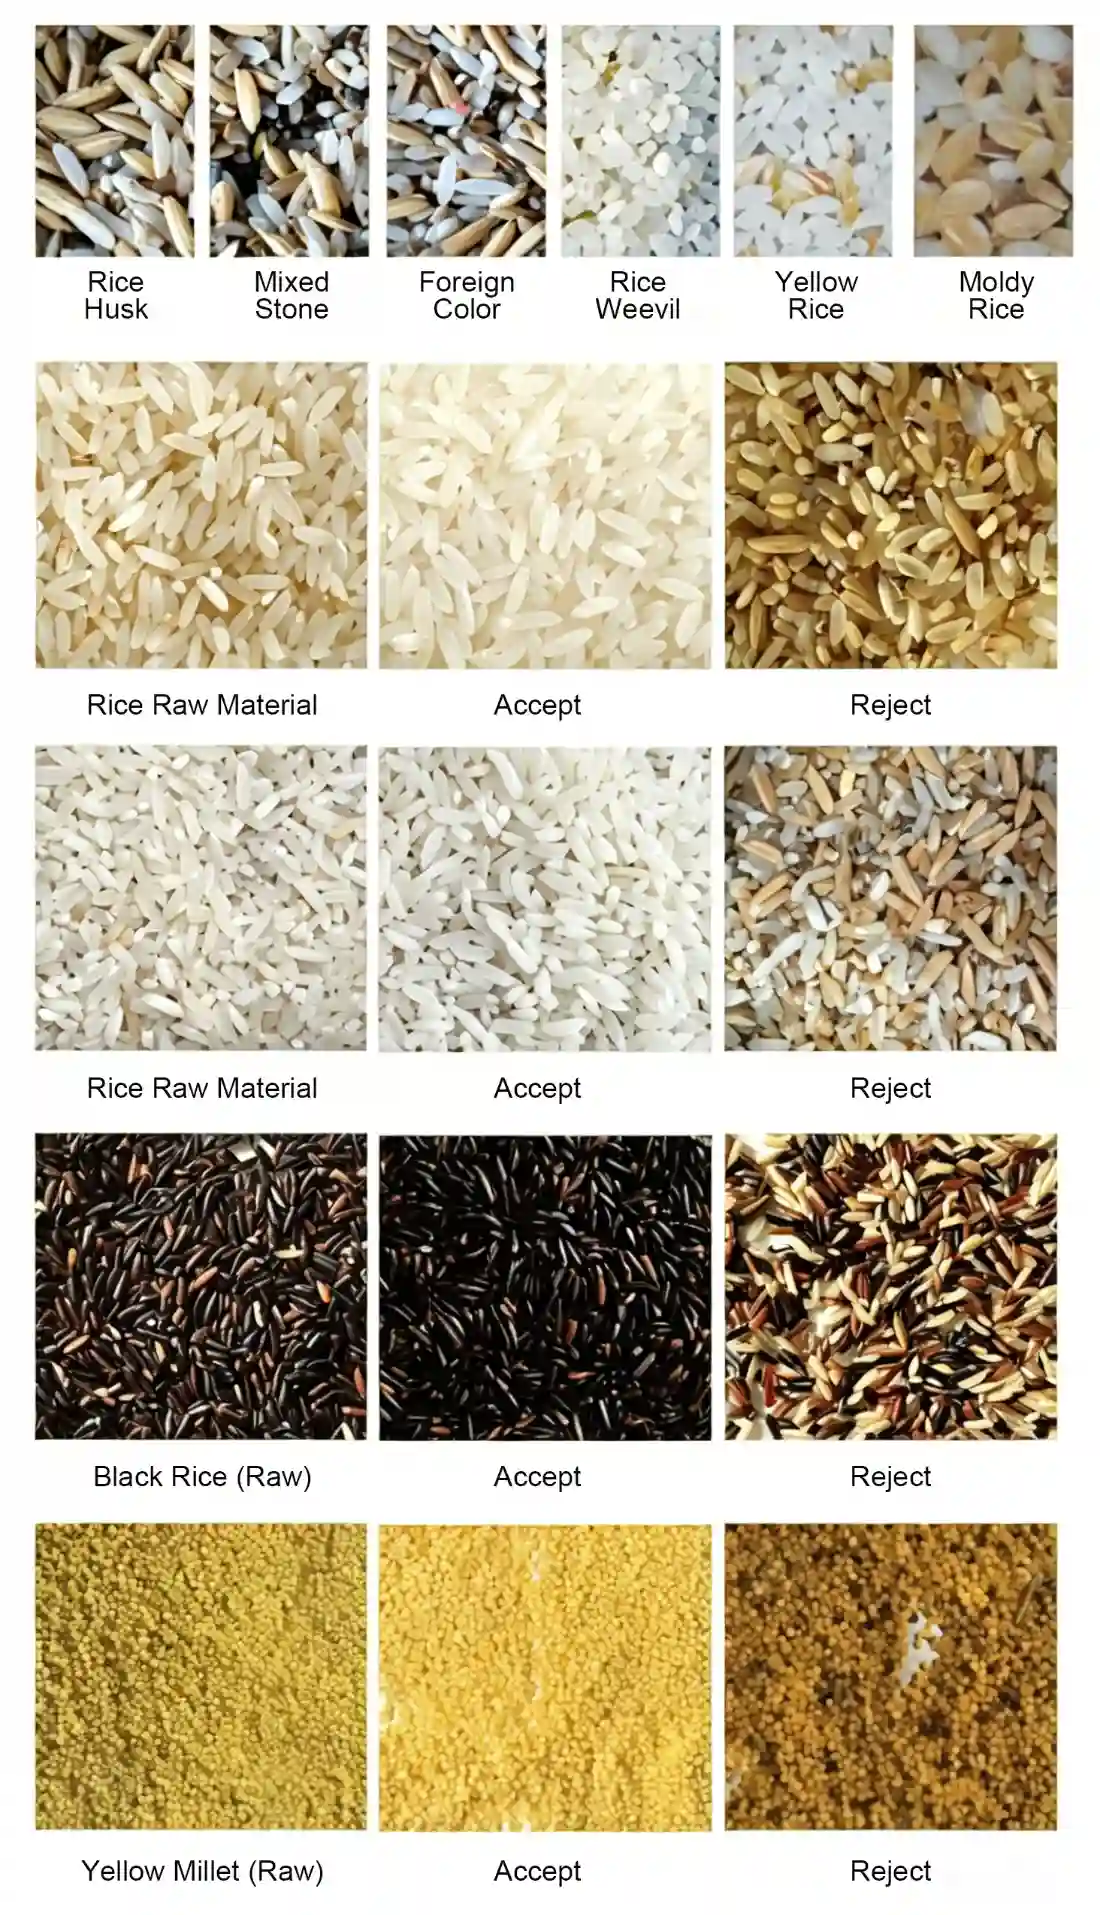
The R MAX high-capacity industrial rice color sorter machine delivers stable and thorough separation performance under continuous large-volume material feeding conditions, coping with various common rice impurities including rice husks, mixed gravel, pest-infested grains, yellow deteriorated grains and moldy particles in bulk raw rice.
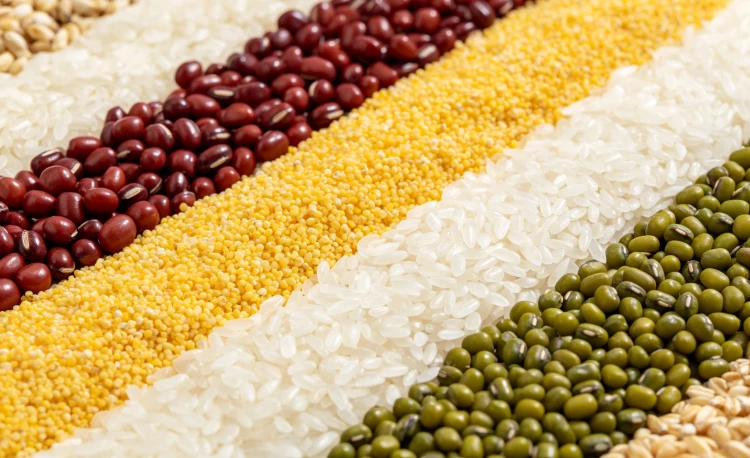
As a multi-purpose industrial sorting device, it not only meets the mass purification demands of conventional polished rice, brown rice and parboiled rice for large rice milling lines, but also supports stable high-throughput sorting processing for specialty black rice and grain crops such as yellow millet. Even under 24-hour uninterrupted heavy-load production, the equipment maintains clean finished grain output and complete interception of defective materials, helping large-scale grain processing bases realize unified quality control for multiple grain varieties on one single sorting unit, reducing supporting equipment investment and overall production management costs.
Service & Technical Support
Full Lifecycle Industrial-Grade Support for R MAX High-Capacity Rice Color Sorter
Tailored for large automated rice milling factories with 24/7 continuous industrial production lines, the R MAX adopts a full-cycle tiered service system to minimize production halt risks and secure stable long-term high-throughput sorting operation for bulk grain processing projects.
1. Pre-Sales Customized Industrial Solution Service
Our senior process engineers analyze your actual raw grain composition, hourly processing capacity target, factory layout and whole-line technological flow to formulate matched R MAX model configuration, air supporting system matching and layout planning schemes. Free grain sorting tests are supported with your local rice samples to verify real sorting purity and reject rate before order confirmation, avoiding equipment mismatch risks for large-scale investment projects.
2. On-Site Commissioning & Professional Technical Training
Professional field engineers carry out full machine installation, pipeline layout, system debugging and Site Acceptance Test (SAT) on your production site. We deliver systematic offline training covering equipment operation methods, standard preventive maintenance specifications, basic fault troubleshooting and routine wearing parts replacement operations, ensuring internal staff can independently operate and manage the high-load sorting unit proficiently. Complete paper and electronic operation manuals are delivered together with the equipment.
3. 7×24 Global Fast Response & Remote Intelligent O&M
Equipped with built-in industrial IoT communication module, R MAX supports one-click remote connection. Our technical team provides remote parameter calibration, real-time operation data monitoring, online fault diagnosis and algorithm remote optimization 24 hours a day. Online response within 10 minutes and preliminary troubleshooting solutions are provided within 4 hours to rapidly eliminate most abnormal alarms without waiting for on-site personnel arrival.
4. Standard Warranty & Lifetime Technical Maintenance
The whole machine enjoys a 12-month quality warranty from the date of on-site acceptance (excluding wearable vulnerable consumable parts such as nozzles, filter elements and light sources damaged by normal wear). After the warranty expires, we provide cost-effective original OEM spare parts via our stable global logistics network, alongside chargeable hardware overhaul services and permanently free software algorithm iteration upgrades, keeping your R MAX equipment always in optimal sorting state during long-period heavy-duty operation.
5. Priority On-Site Emergency Rescue Service
For complex failures that cannot be solved remotely, we arrange overseas after-sales engineers for targeted on-site maintenance according to emergency priority, effectively resolving sudden equipment failures and cutting downtime losses for your uninterrupted industrial rice production lines. Regular periodic return visits are also arranged to inspect running status and eliminate potential hidden troubles in advance.
6. Dedicated Exclusive Project Manager
Each R MAX large sorting equipment project is assigned an exclusive project manager as your unified docking person throughout the whole cooperation cycle, coordinating all technical, delivery and after-sales links to realize one-stop hassle-free service for large grain industrial customers.
FAQS
-
Can the R Max rice color sorter support 24/7 uninterrupted continuous operation inside fully automated large-scale rice milling factories?
The R Max adopts a thickened industrial reinforced overall frame structure matched with an optimized multi-channel anti-block feeding system. The whole mechanical structure is calibrated and tested targeting long-cycle mass grain processing scenarios, which perfectly meets the stable round-the-clock continuous sorting demands of automated large rice production lines without frequent shutdown caused by structural fatigue or material blockage.
-
When the equipment is running at ultra-high material throughput, will the sorting system produce a higher mistaken rejection rate of intact qualified rice and cause raw material economic loss?
The machine is equipped with a synchronous linkage high-speed jet ejection balance system. It matches the material falling speed under large flow volume in real time, locking the mistaken rejection proportion of intact good grains within an extremely low and stable numerical range. It effectively reduces raw material waste and improves the finished rice yield rate for bulk industrial rice processing.
-
Can the R Max automatically cope with minor moisture content fluctuations of incoming raw rice during daily continuous production?
Built-in dedicated intelligent moisture compensation algorithm can dynamically adjust the optical identification threshold in real time when raw rice has normal small-range moisture deviation. It avoids sorting precision drift triggered by the change of rice surface gloss and refraction, maintaining stable impurity removal accuracy under unstable raw material status in actual rice mill production.
-
In terms of daily routine maintenance work, is the operation burden of R Max consistent with the small-sized standard R entry-level model?
Compared with the basic small R model, users only need to add regular weekly cleaning for the air filter component of the R Max high-flow air circuit system. All daily inspection, module checking, routine wearing parts replacement and core equipment maintenance processes are completely unified with the entry-level R series, without bringing extra complicated maintenance work for factory operation staff.
We strictly control the production quality of each product and meticulously process every item.
Related Products